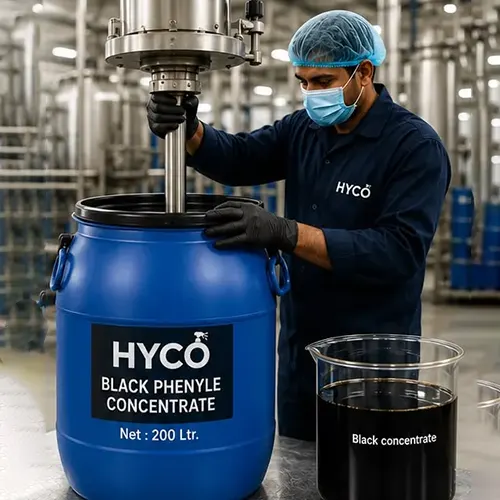
Alok Industries, introduces Hyco Black Phenyl Concentrate in Indore, with strong cleaning performance, consistent quality and manufacturer direct supply to give you a hassle free service. We are offering premium quality concentrated formulation developed for manufacturers, distributors, wholesalers, and entrepreneurs who are thinking to produce high-quality Black Phenyl with a strong cleaning performance and cost effective efficiency. We manufacture using premium raw material to produce our product without compromising its quality. Our product delivers powerful floor cleaning emulsion, and quality in every batch. We have two ranges for Black Phenyl Concentrate, that is –
Alok Industries is commonly known as the most transparent and trustworthy Black Phenyl Concentrate Manufacturers in Madhya Pradesh. We are here to give our most reliable and economical formulation suitable for everyday floor cleaning with the dilution ratio 1:9
For a better and reliable economical formulation follow–
Our premium formulation is designed for superior cleaning performance, improved fragrance retention, and enhanced product stability. We recommend dilution ratio 1:19
For a better and reliable economical formulation follow–
If you are thinking of making ready to use black phenyl then you are at the right place. As we have our own manufacturing so we are capable of giving you flexible dilution based Black Phenyl Concentrate. As per being a responsible Black Phenyl Concentrate Suppliers in Indore, our recommended dilution ratios are developed to provide the ideal balance of cleaning performance, appearance, and stability. You can adjust the quantity of water according to your target market and requirement. You can also adjust the price that best suits your customers. For optimum performance, we recommend following the suggested dilution ratios.
HYCO Black Phenyl Concentrate has a deep black appearance inside the container. After dilution and preparation, it retains its premium quality, and when the final product is mixed with water during floor cleaning, it forms a milky-white emulsion. We have dealt with hundreds of dealers and become the most famous Black Phenyl Concentrate Wholesalers in India. The natural colour transformation helps the product spread evenly across, and is a hallmark of a high-quality phenyl formulation.
Our formulation is developed with a balanced pH to provide effective cleaning while maintaining product stability, consistent performance, and excellent shelf life. Every batch we deliver is produced under strict quality control to ensure reliable quality and uniform results.
Use RO water, DM water, or soft water whenever possible for the best results. Add the concentrate slowly while stirring continuously to ensure proper mixing. Continue mixing thoroughly until the solution becomes completely uniform, then allow it to stabilize before filling. Finally, fill the prepared solution only into clean, dry HDPE or PET containers to maintain product quality and prevent contamination.
Our products are full of benefits that consists these key-features–
* Highly Concentrated Formula
* Powerful Floor Cleaning
* Balanced pH Formulation
* Advanced Reagent Technology
* Deep Black Concentrate
* Forms Milky-White Emulsion During Use
* Long-Lasting Fragrance
* Stable & Uniform Formulation
* Easy to Dilute
* Cost-Effective Manufacturing
* Excellent Shelf Stability
* Consistent Batch Quality
We supply premium-quality Hyco Black Phenyle Concentrates that enable you to manufacture and market worthy products under your own brand name. All you have to do is simply dilute the concentrate, package it in your preferred bottles, apply your own branding, and sell it according to your business requirements.
We give manufacturer direct supply so that you can create & sell under your own brand, we offer free delivery on orders of 200-litre barrels, we use premium quality raw materials, technical mixing & manufacturing guidance, bulk supply across India, deliver consistent batch quality and Secure industrial packaging and reliable business support
We are happy to serve everyone who wants to work with us. We mainly focus on providing our services to Cleaning Product Manufacturers, Distributors & Wholesalers, Retail Brand Owners, Hotels, Hospitals, Schools & Colleges, Offices, Commercial Buildings, Factories & Warehouses, Public Institutions and Facility Management Companies.
Store the concentrate in a cool, dry place and keep the container tightly closed after each use to preserve its quality. Avoid keeping it in direct sunlight and heat, as these conditions may affect product performance. During both storage and dilution, protect the concentrate from contamination by using clean equipment and handling it carefully. Always keep the product out of the reach of children.
Kindly follow all the recommendations to keep your business safe and secure.
To manufacture premium-quality cleaning and hygiene products that deliver superior performance, promote healthier environments, and provide reliable, affordable solutions for homes, businesses, and institutions.
To become a leading and trusted cleaning products brand by continuously innovating, maintaining the highest quality standards, and delivering effective hygiene solutions that improve everyday living.